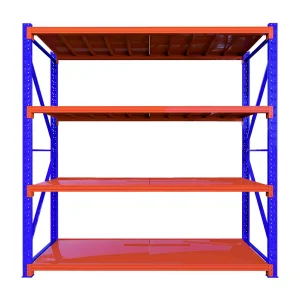
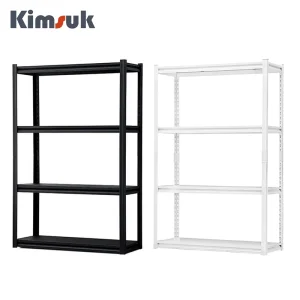
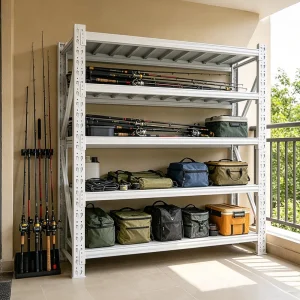
Explore our elite range of engineered storage equipment manufactured to optimize industrial warehouse workflows and supply chain fulfillment.

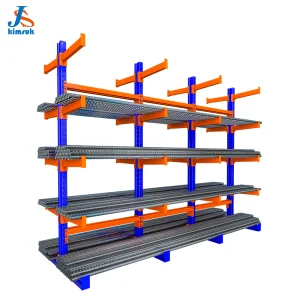


A Comprehensive Analysis of Modern Supply Chain Infrastructure, Manufacturing Excellence, and Strategic Global Sourcing from China.
In the contemporary era of hyper-accelerated global trade and e-commerce expansion, the demand for robust shipping supplies and industrial storage systems has reached unprecedented heights. Supply chain managers, third-party logistics (3PL) providers, and industrial conglomerates are continuously challenged to optimize floor space, reduce fulfillment latency, and guarantee absolute structural integrity during cargo handling and transit.
As the undisputed manufacturing powerhouse of the world, China has positioned itself as the premier sourcing destination for heavy-duty storage equipment. Chinese manufacturing clusters combine advanced metallurgical science, precision automated stamping, robotic welding, and rigorous quality assurance protocols to deliver world-class infrastructure that complies with international safety standards such as RMI, FEM, and AS/NZS.
Sourcing shipping supplies and warehouse racking systems directly from specialized Chinese manufacturers unlocks exceptional strategic advantages. Beyond cost efficiencies derived from localized raw material supply chains and economies of scale, top-tier factories offer unparalleled OEM and ODM customization capabilities.
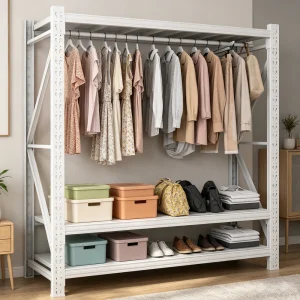
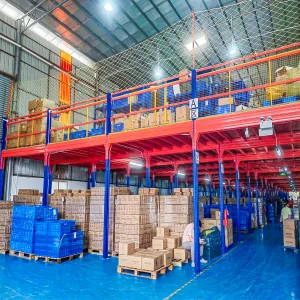
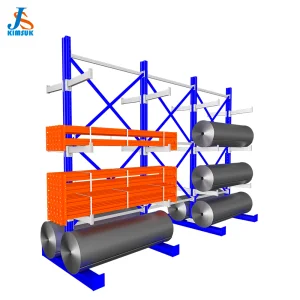
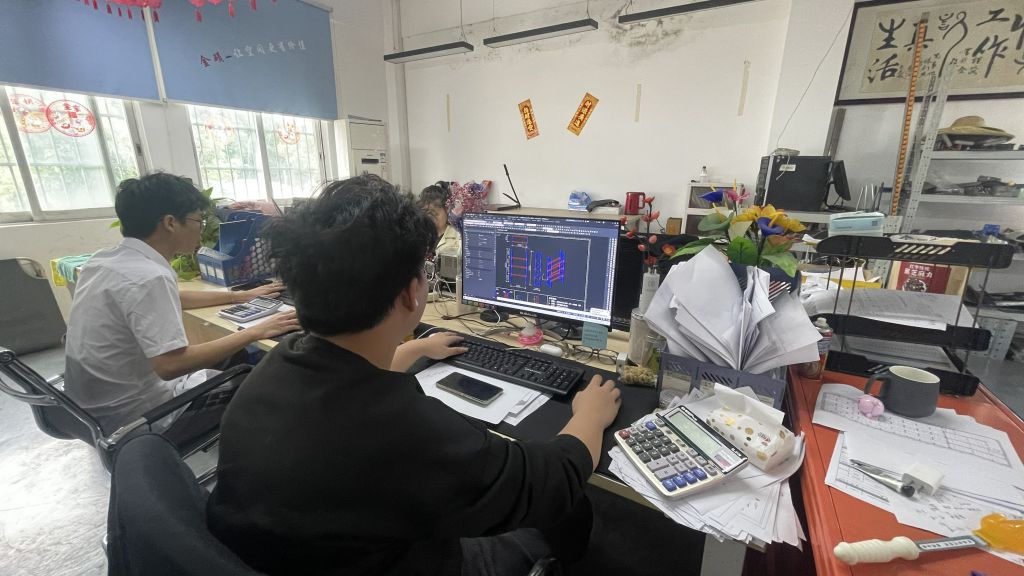
Whether enterprise clients require seismic-rated pallet racks, specialized cantilever systems for raw lumber and steel pipes, or multi-tier mezzanine floors to triple usable warehouse cubic capacity, Chinese engineering teams provide comprehensive CAD/BIM layout planning, rapid prototyping, and end-to-end export project execution.
Your Trusted Partner in Industrial Storage Systems and Shipping Supply Solutions Since 2016.
Shenzhen Kimsuk Storage Equipment Manufacturing Co., Ltd. was established in 2016 and specializes in the design, manufacturing, and global supply of high-quality warehouse storage equipment. With a factory area of 18,500㎡, we provide professional storage solutions for warehouses, factories, logistics centers, and industrial applications worldwide.
With an annual export revenue of approximately $12 million and 8 years of export experience, Kimsuk has accumulated more than 14 years of industry experience in warehouse racking and storage equipment manufacturing. Our products include pallet racks, heavy duty racks, cantilever racks, mezzanine floors, shelving systems, and customized storage solutions.
We implement strict quality control procedures throughout the production process. Our quality inspection system includes raw material inspection, welding quality checks, surface treatment inspection, dimensional accuracy testing, load-bearing tests, and final product performance evaluation. Each product undergoes professional inspection using equipment such as laser measurement tools, load testing machines, coating thickness gauges, and precision measuring instruments.
Our quality control team consists of 45 experienced inspectors who ensure every shipment meets international standards and customer requirements. We have established a professional manufacturing and trading system supported by advanced production equipment, experienced engineers, and reliable supply chain management.
Our main markets include North America, Europe, Southeast Asia, the Middle East, Australia, and South America. We cooperate with more than 850 supply chain partners, allowing us to provide stable raw materials, efficient production capacity, and competitive delivery solutions.
Our customers include logistics companies, e-commerce warehouses, manufacturing enterprises, retail distributors, third-party logistics providers, and industrial project contractors. We provide complete storage solutions from planning and design to manufacturing and installation support.
Kimsuk has a strong research and development capability with an experienced engineering team focused on product innovation and structural optimization. We offer customized options including rack dimensions, load capacities, colors, configurations, materials, and complete warehouse storage layouts.
In the past year, we launched more than 120 new products and improved existing storage systems to meet changing market demands. Our R&D department consists of 18 professional engineers specializing in storage equipment design, product development, and customized engineering solutions.
Shenzhen Kimsuk Storage Equipment Manufacturing Co., Ltd. is committed to delivering reliable, efficient, and innovative warehouse storage solutions to customers around the world through advanced manufacturing technology, strict quality management, and continuous product improvement.
Precision engineering empowered by state-of-the-art automated machinery and rigorous quality control workflows.
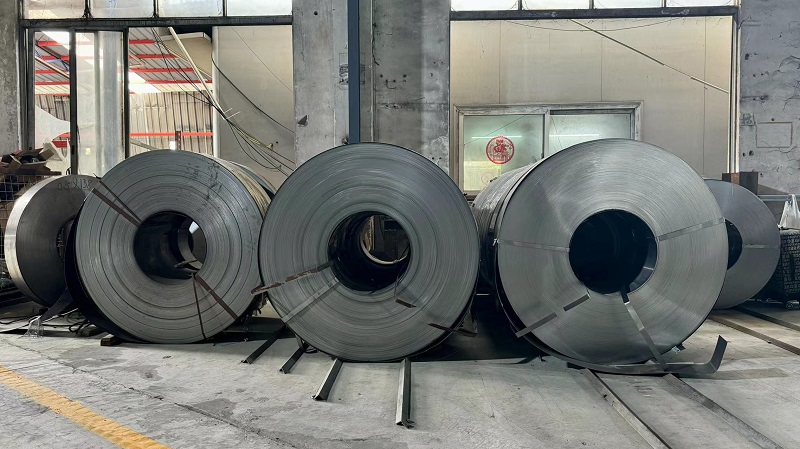
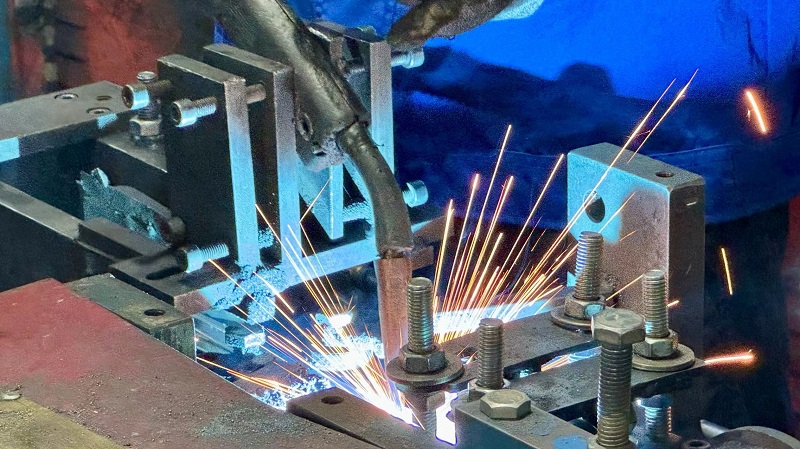
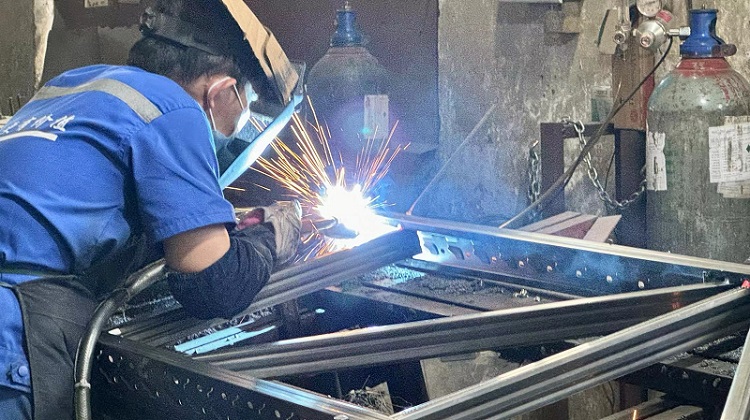
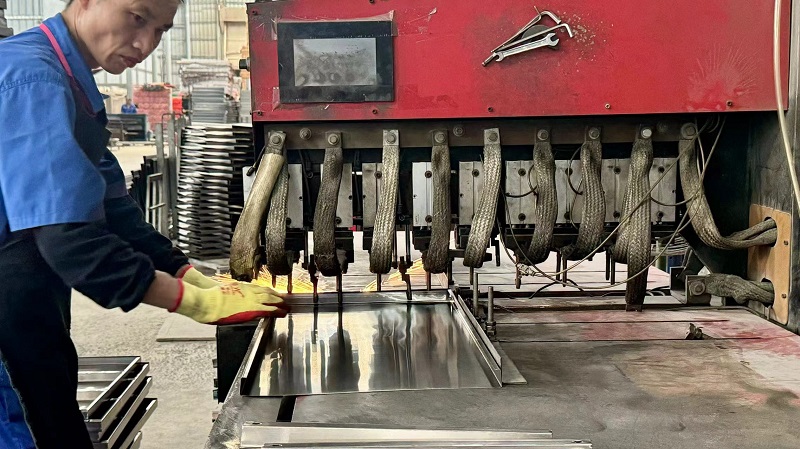
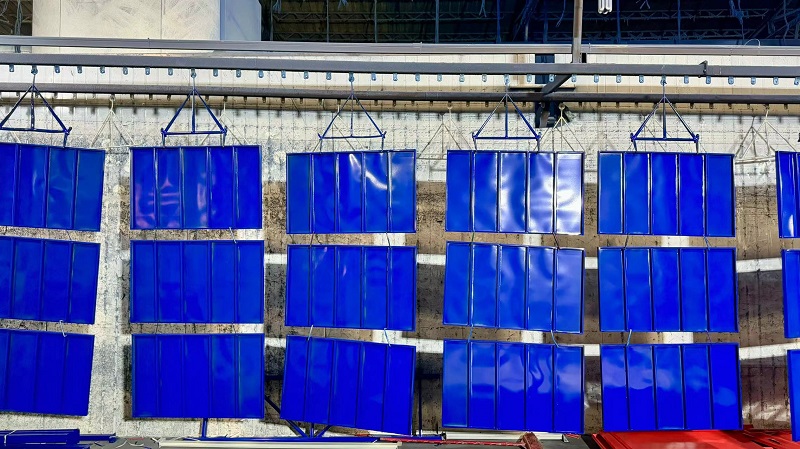
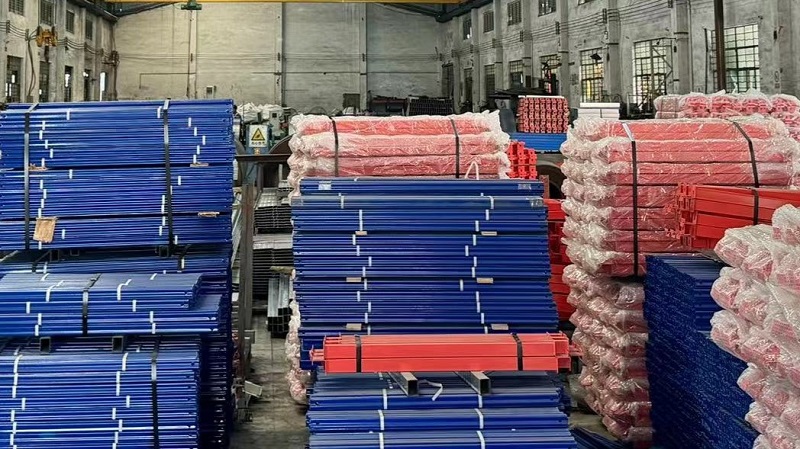
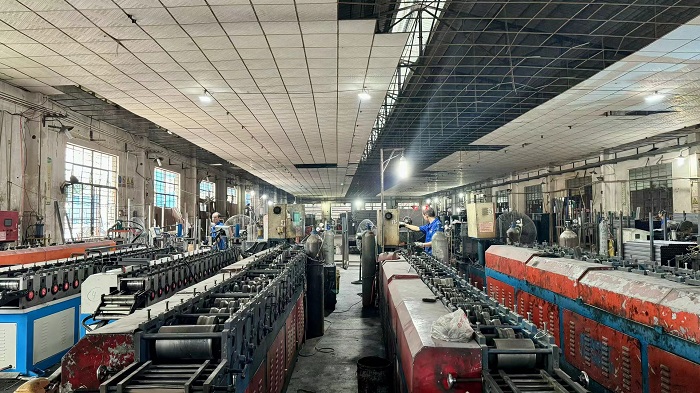
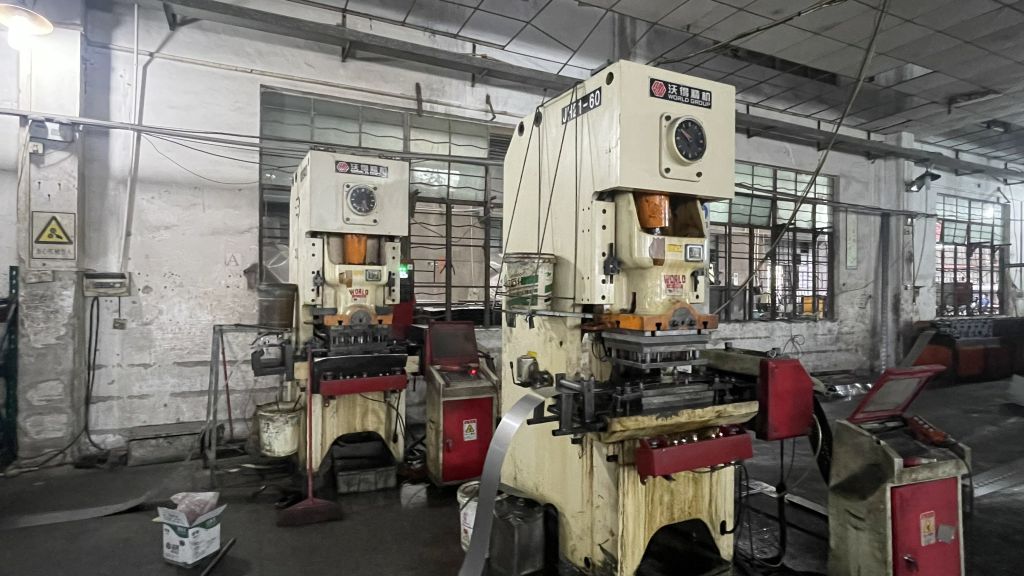
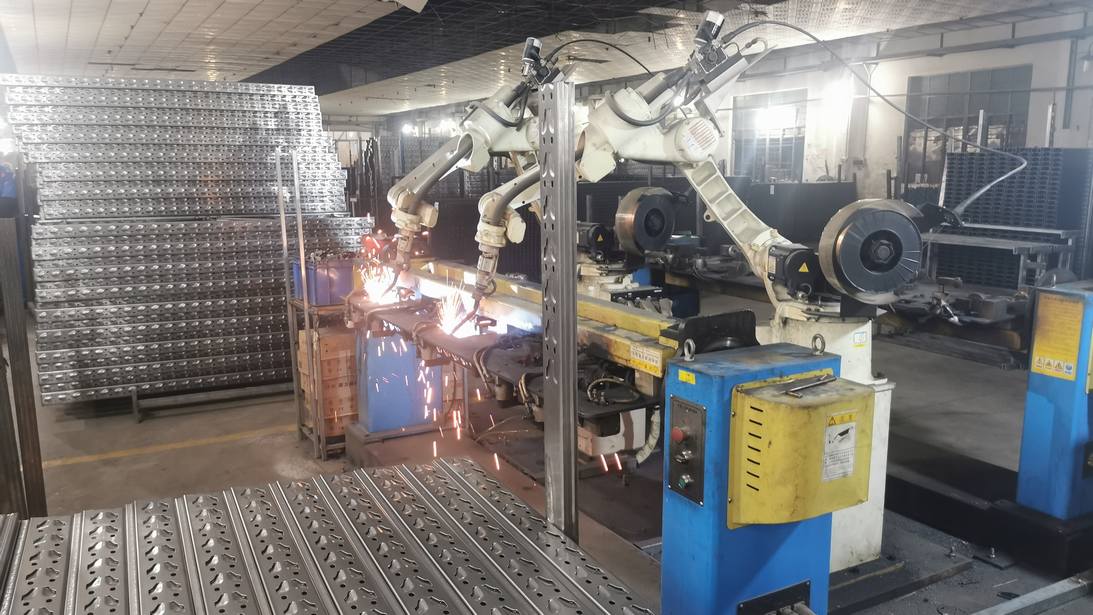
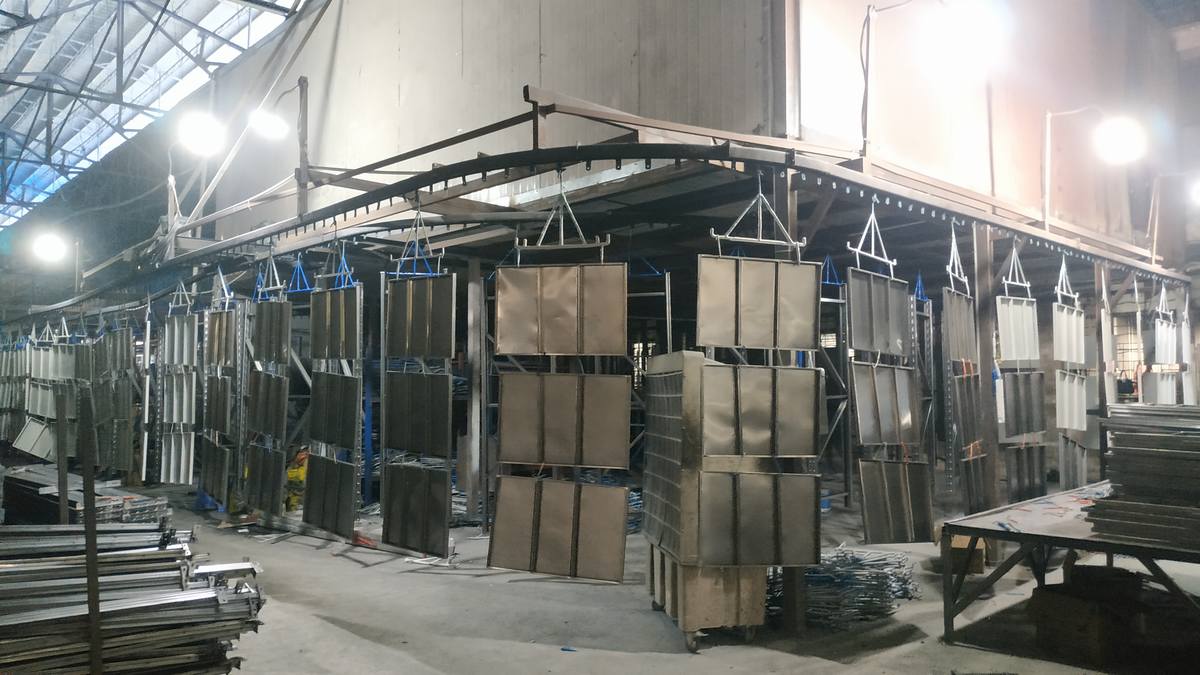
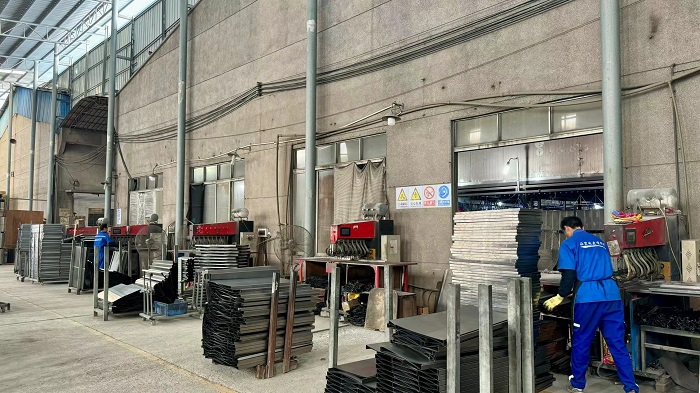
Discover our specialized heavy-duty cantilever racks, selective pallet racking systems, and modular industrial shelving units.


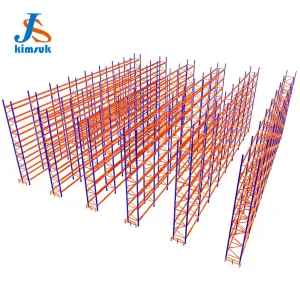
Expert answers regarding importing shipping supplies, warehouse storage racks, and custom manufacturing from China.
Kimsuk combines over 14 years of manufacturing expertise with an 18,500㎡ advanced production facility. We maintain stringent quality control with 45 dedicated inspectors, use precision machinery like automated stamping and robotic welding lines, and export $12M+ annually to over 850 global supply chain partners.
Yes. Our R&D department features 18 professional engineers specializing in structural optimization and custom engineering. We provide tailor-made dimensions, load capacities ranging from 100kg to 5000kg per layer, specialized coatings, and complete CAD/BIM warehouse layout designs.
Every batch undergoes rigorous evaluation using laser measurement tools, load testing machines, coating thickness gauges, and precision measuring instruments. We inspect raw materials, welding integrity, surface powder coating, and dimensional tolerances prior to export packaging.
We actively export to North America, Europe, Southeast Asia, the Middle East, Australia, and South America. Thanks to our robust supply chain network of 850+ partners and efficient manufacturing lines, we guarantee stable production schedules and competitive delivery solutions worldwide.
 Kimsuk Storage