Explore our engineered high-capacity storage racks and heavy-duty shelving units designed to optimize global warehousing, e-commerce fulfillment centers, and industrial shop floors.


In the realm of modern supply chain ecosystems, the symbiosis between advanced material handling equipment, forklift accessories, and structural warehouse racking determines enterprise operational efficiency. Adhering to strict Google E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) standards, this report analyzes manufacturing excellence, macroeconomic trends, and procurement strategies.
Shenzhen Kimsuk Storage Equipment Manufacturing Co., Ltd. was established in 2016 and specializes in the design, manufacturing, and global supply of high-quality warehouse storage equipment. With a factory area of 18,500㎡, we provide professional storage solutions for warehouses, factories, logistics centers, and industrial applications worldwide.
With an annual export revenue of approximately $12 million and 8 years of export experience, Kimsuk has accumulated more than 14 years of industry experience in warehouse racking and storage equipment manufacturing. Our products include pallet racks, heavy duty racks, cantilever racks, mezzanine floors, shelving systems, and customized storage solutions.
We implement strict quality control procedures throughout the production process. Our quality inspection system includes raw material inspection, welding quality checks, surface treatment inspection, dimensional accuracy testing, load-bearing tests, and final product performance evaluation. Each product undergoes professional inspection using equipment such as laser measurement tools, load testing machines, coating thickness gauges, and precision measuring instruments.
Our quality control team consists of 45 experienced inspectors who ensure every shipment meets international standards and customer requirements. We have established a professional manufacturing and trading system supported by advanced production equipment, experienced engineers, and reliable supply chain management.
Precision engineering backed by state-of-the-art machinery ensures structural integrity, optimal load distribution, and durable surface finishes for all material handling structures.
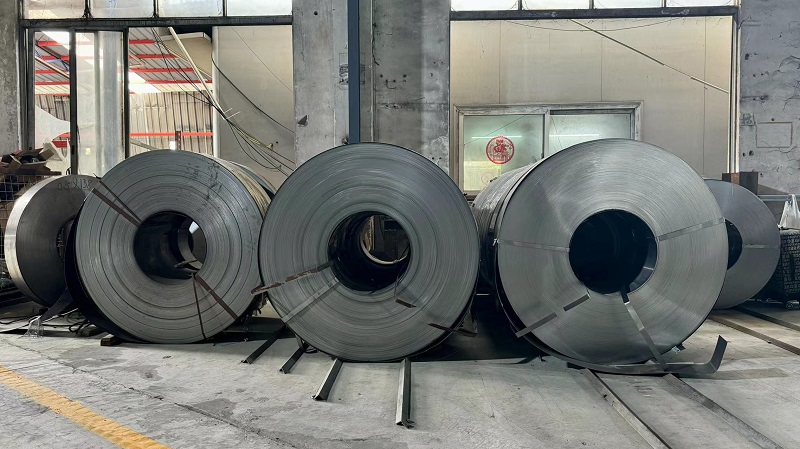
Sourcing premium-grade structural steel from certified mills.
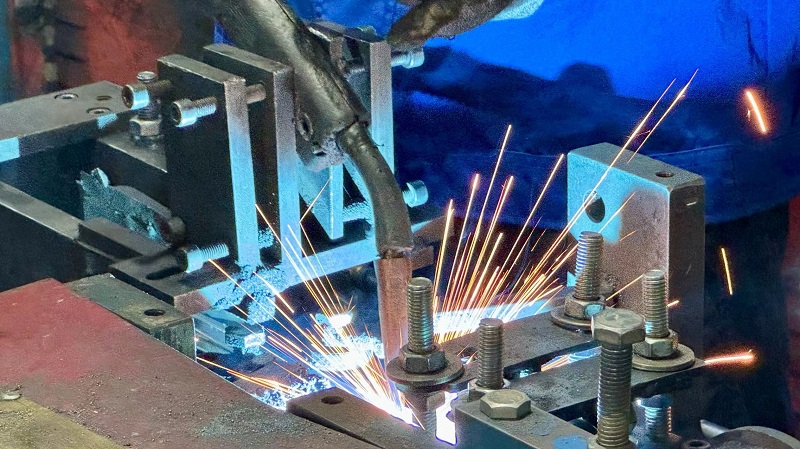
High-precision stamping for exact component dimensions.
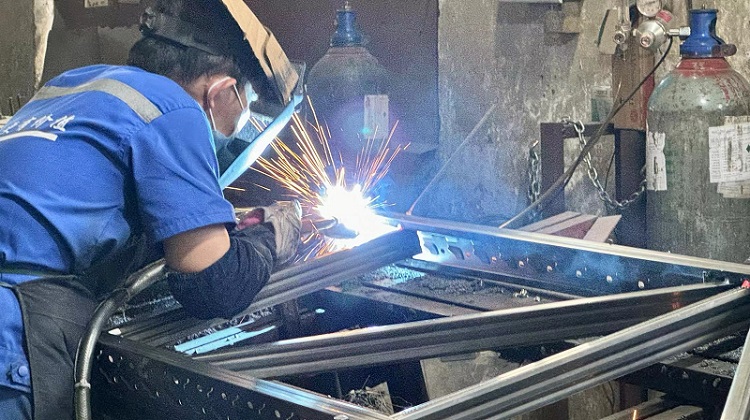
Advanced robotic and certified manual welding for maximum load tolerance.
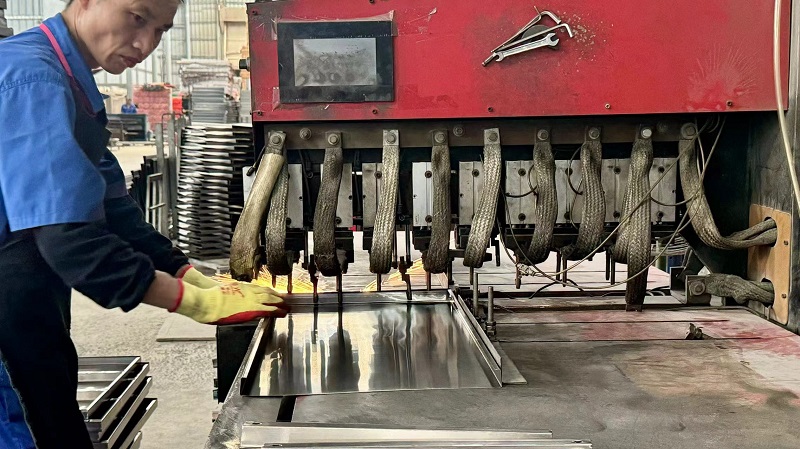
Computer-numerical-control punching for structural alignment.
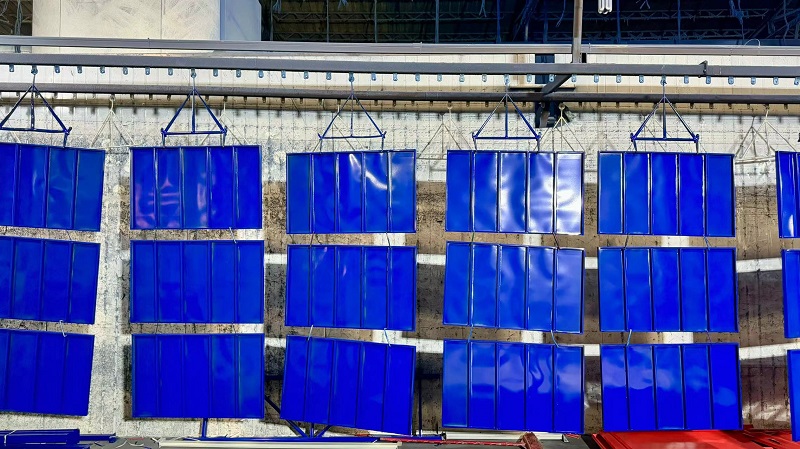
Electrostatic powder coating line ensuring corrosion resistance.
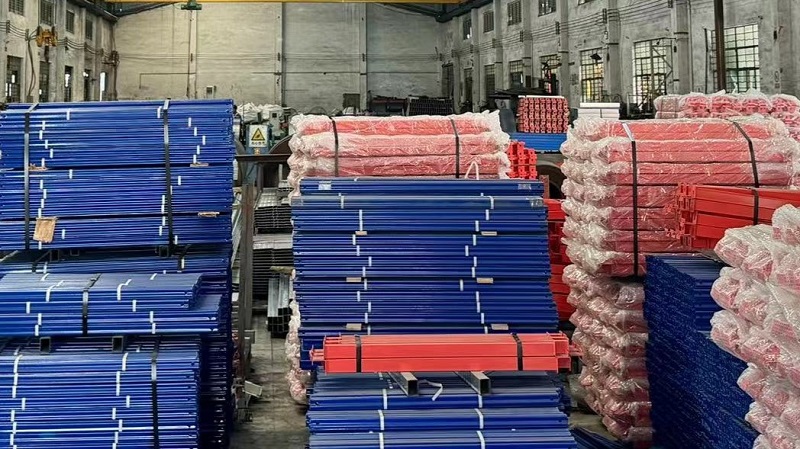
Secure export-grade packaging for safe international transit.
Our facility is equipped with heavy industrial equipment designed to scale high-volume production without compromising strict tolerances.
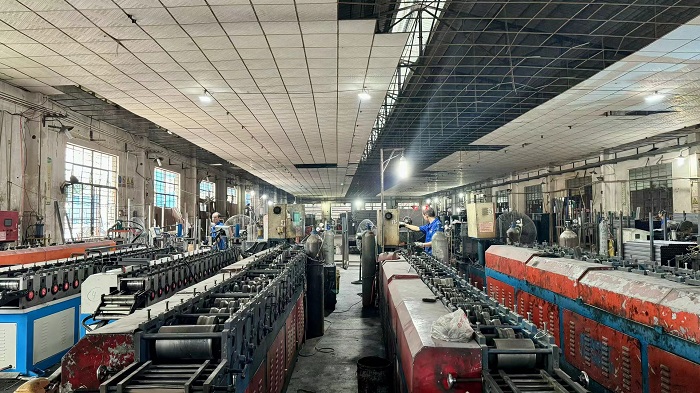
Heavy tonnage presses for structural components.
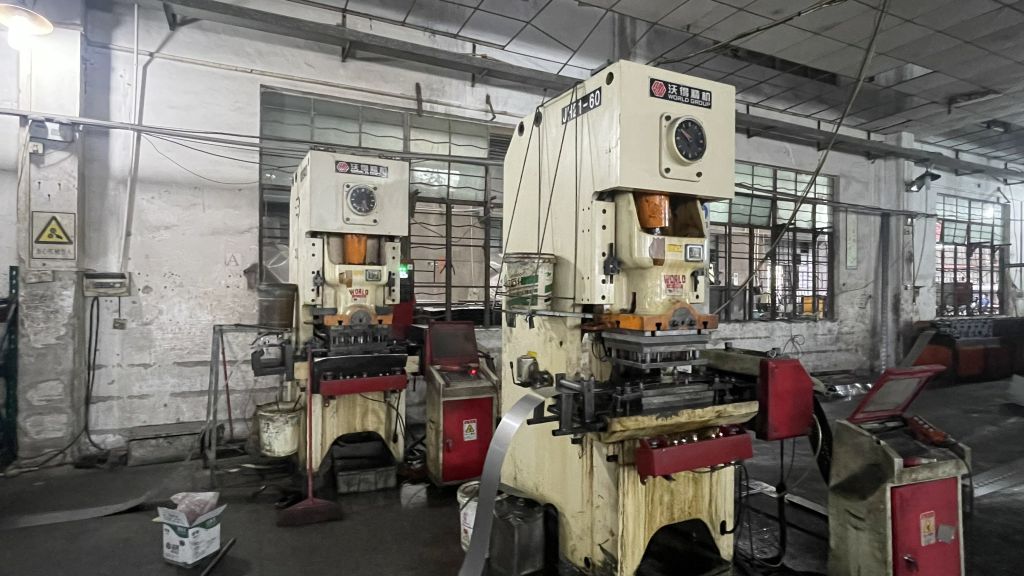
Advanced piercing technology for seamless joints.
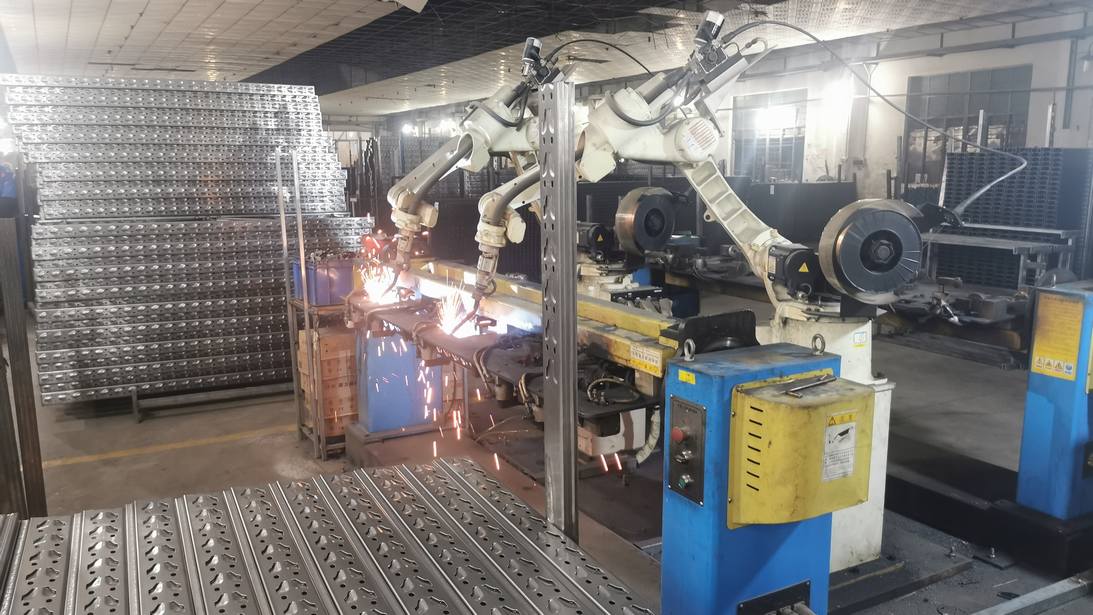
High-efficiency automated welding stations.
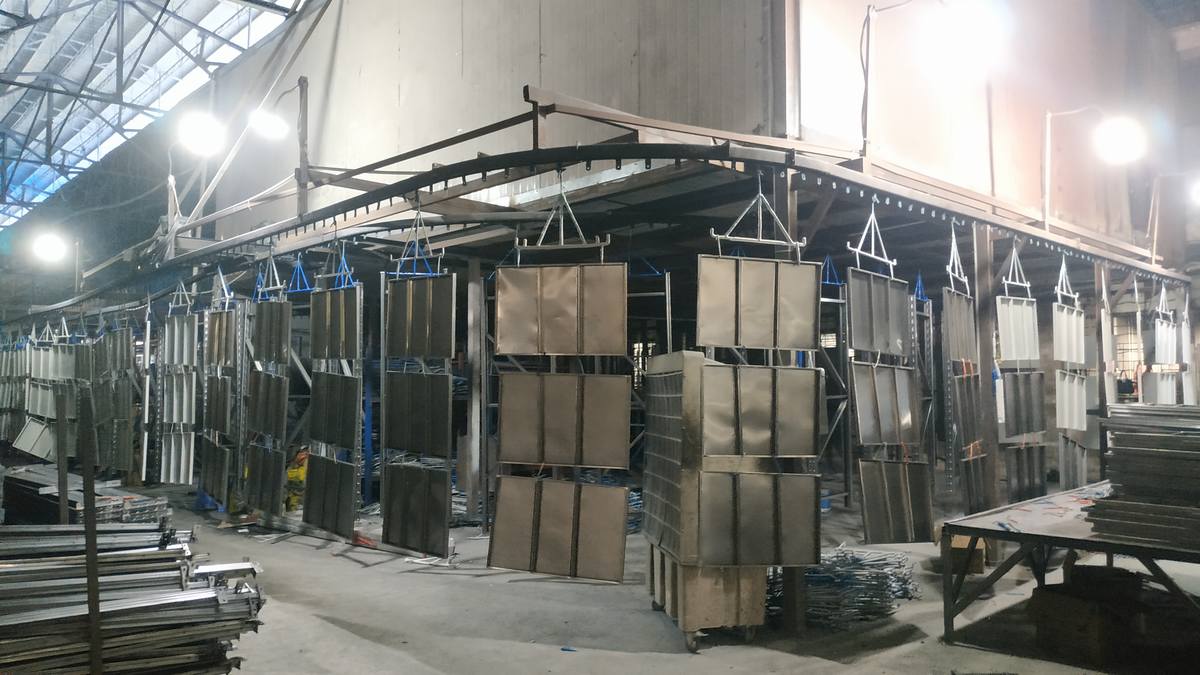
Continuous conveyorized powder coating system.
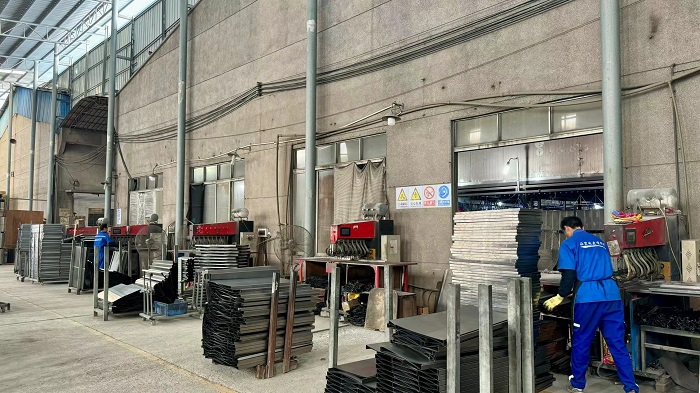
High-speed automated perforation units.
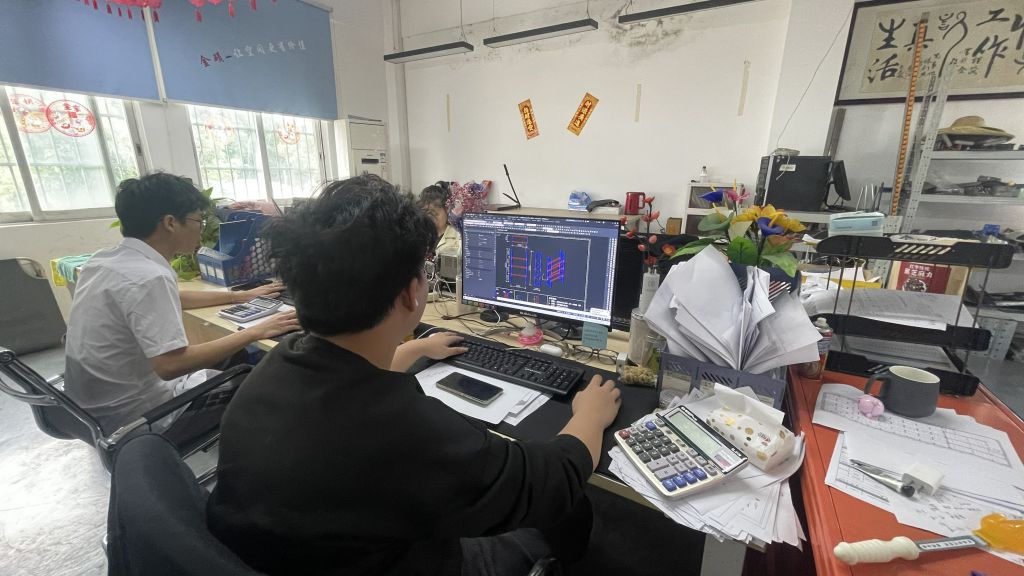
Engineering simulation and structural FEA analysis.
As global supply chains navigate rapid e-commerce expansion, automated storage and retrieval systems (ASRS) and specialized forklift attachments are experiencing unprecedented demand. Chinese manufacturing hubs have taken the lead by integrating advanced material sciences, IoT-enabled inventory tracking, and highly adaptable modular architecture.
International enterprises spanning North America, Europe, Southeast Asia, and South America require robust logistics infrastructure. Our solutions bridge the gap between high-density storage needs and rapid SKU throughput, ensuring maximum cubic utilization of warehouse space.
The convergence of automated guided vehicles (AGVs), smart forklift accessories, and precision-engineered racking systems represents the future of warehousing. Modular designs allow businesses to scale operations efficiently with minimal downtime.
Maximize your vertical space with our certified mezzanine platforms, heavy-duty pallet racks, and modular industrial shelving configurations.

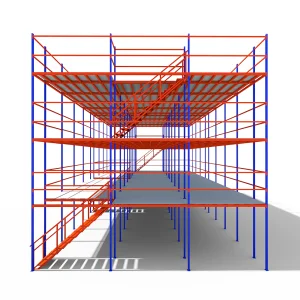

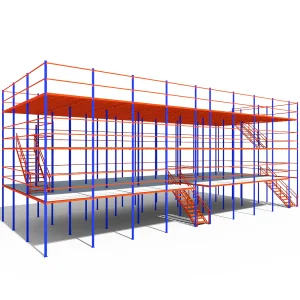
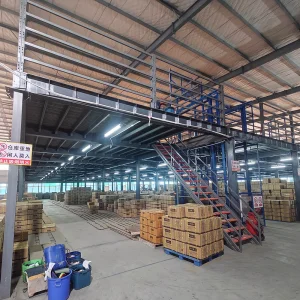
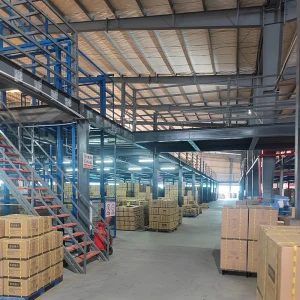
Expert answers regarding global sourcing, custom engineering, and structural quality standards for industrial storage equipment.
Chinese manufacturers offer an optimal combination of robust industrial supply chains, advanced automated production equipment (such as robotic welders and precision stamping lines), and cost-effective scaling capabilities. Companies like Shenzhen Kimsuk combine over 14 years of engineering expertise with strict ISO-compliant quality control to deliver global-standard products.
All structural storage units undergo rigorous load-bearing tests using hydraulic pressure machines, laser measurement tools for deflection analysis, and coating thickness gauges. Quality control teams perform batch inspections to guarantee safe operating loads ranging from 500kg up to 5000kg per tier.
Yes. Professional manufacturers provide complete customized engineering services including tailored dimensions, adjustable tier heights, specific RAL color coatings, and specialized seismic or guardrail configurations tailored to e-commerce fulfillment centers and 3PL warehouses.
Major export destinations include North America, Europe, Australia, the Middle East, and South America. Products are meticulously packed using export-grade steel banding, protective edge guards, and moisture-resistant wrapping to ensure damage-free international ocean and land freight delivery.
 Kimsuk Storage